close
Choose Your Site
Global
Social Media
Views: 0 Author: Site Editor Publish Time: 2026-08-06 Origin: Site


Picking the right paper cup manufacturing equipment controls your business profits. It also affects how many cups you can make. You must match your manufacturing equipment to your company size. This applies to small startups and big factories. Every good choice of manufacturing equipment depends on four main rules:
Evaluation Criterion | Operational Impact |
|---|---|
Production Capacity | Matches machine speed to your sales goals |
Size Flexibility | Helps swap molds fast for different cup sizes |
Material Compatibility | Works with single PE, double PE, and PLA coatings |
Sealing Technology | Fixes side seams with heat or ultrasonic tools |
You save money by checking these details early. You will also stop manufacturing equipment breakdowns and avoid lost time.
Pick machines using your daily cup goals and budget.
Real cup output is less than top machine speed.
Ultrasonic sealing saves power. It works great on green paper covers.
Modern open-cam drives reduce fix time. They work better than old chains.
Smart sensors remove bad cups. This keeps the final products good.
Think about long-term repair costs. Do not just look at low initial prices.
Table of Contents
You must match machine capacity directly to your business operational goals. Selecting appropriate gear prevents costly operational bottlenecks. You optimize your capital allocation when you match plant scale with precise machine output levels.
Startups face unique constraints regarding capital efficiency and physical space. You must select equipment that balances initial costs against target production volumes.
Entry-level machinery provides straightforward mechanical designs for small facilities. Manual units require significant physical labor. These manual systems yield a daily output of 1,500 to 2,000 cups. You can also deploy entry-level desktop units for micro-businesses or educational demonstrations. Desktop units run at speeds of 10 to 20 cups per minute, but they lack durability for continuous operations.
Semi-automatic machines serve startups entering small-scale regional distribution networks. Operators manage semi-automatic models easily. These machines deliver variable speeds between 30 to 60 cups per minute. They deliver a daily output of 5,000 to 10,000 cups. However, semi-automatic units require moderate labor intervention and display variable processing speeds during extended runs.
Capital requirements vary across entry-level machinery options:
Machine Category | Initial Capital Requirement | Daily Output Capacity | Operational Characteristics |
|---|---|---|---|
Manual Units | $3,000 to $5,000 | 1,500 to 2,000 cups | Heavy manual labor required |
Semi-Automatic Units | $5,000 to $8,000 | 5,000 to 10,000 cups | Moderate labor intervention |
Entry-Level Standard | $8,000 to $15,000 | 30 to 50 cups per minute | Baseline continuous output |
Fully Automatic Units | $10,000 to $12,000 | 50,000 to 80,000 cups | Minimal human labor needed |
A basic conversion-only entry setup requires roughly $25,000 in capital expenditures. This setup relies entirely on pre-printed and die-cut blanks. Full vertical integration demands a capital investment ranging from $200,000 to $500,000. You also need an additional $30,000 to $50,000 for your initial raw material inventory. Raw materials account for 70% to 75% of your total production costs. Operating expenses like power, facility rent, and operator labor comprise 10% to 15% of your budget. Small operations maintain an average gross margin of 15% to 25%. However, small setups face material waste rates over 15% and incur 30% to 40% higher overhead per cup. These scale inefficiencies often extend your practical break-even timeline well beyond 24 months.
Mid-scale commercial plants require balanced automation, higher output speeds, and mechanical endurance. You target broader distribution markets with this operational setup.
Medium-speed standard models, like the CM100, target growing business ventures. These systems require an initial investment of $15,000 to $35,000. The forming units operate reliably at speeds between 70 to 90 cups per minute. You benefit directly from low power consumption and uncomplicated mechanical maintenance during standard daily shifts.
Commercial operations demand quick adaptation to changing customer orders. Medium-speed automatic forming units support fast mold changeovers across standard volume sizes. Operators switch tooling components to handle diverse single and double PE container profiles. This flexible tooling keeps your plant agile and minimizes costly downtime between production cycles.
Industrial manufacturers require heavy-duty manufacturing equipment built for round-the-clock commercial output. High-speed systems eliminate human intervention and maximize overall facility throughput.
High-speed automatic units deliver rapid output with advanced motion controls. Servo-driven machinery delivers clear performance benefits:
Fully automated systems require very little human labor daily.
Fast machines make 60 to 150 cups every minute.
Servo-driven feeders align materials within ±0.2 mm precisely.
Automatic lubrication systems cut manual repair hours by 80%.
High-volume plants link high-speed forming units directly to end-to-end automated packaging systems. The machinery manages product transport, tallying, and stacking smoothly. The automated lines seal and box finished goods without physical operator involvement.
Metric Aspect | Rated Machine Speed | Actual Operational Yield Efficiency |
|---|---|---|
Definition | Maximum theoretical speed under ideal lab conditions | Real-world output produced during actual factory shifts |
Example Output | 80 cups per minute | 65–70 cups per minute (over an 8-hour shift) |
Influencing Factors | Manufacturer specification / Ideal lab settings | Paper quality, operator expertise, and warm-up duration |
Non-productive operational factors lower your actual operational yield:
Equipment debugging and tooling adjustments
Scheduled machine maintenance and sudden breakdowns
Operational or operator handling issues
Inconsistencies and variations in raw materials
You track actual yield using a simple formula: yield = good units / total units x 100. Target benchmarks ensure continuous output throughout your daily facility shifts.

Different container designs require flexible production systems. Single and double-wall beverage cups demand precise size tolerances for proper stacking.
Modern horizontal manufacturing equipment features convenient slide-out or drawer-type mold carriers. An efficient operating crew performs a complete mold size transition in less than 20 minutes.
Polyethylene coatings effectively protect paperboard fibers against moisture penetration. Standard single and double PE materials form smoothly under standard thermal heating settings.
PLA exhibits higher brittleness and thermal sensitivity than traditional PE coatings. Heat-sealing PLA demands precise temperature regulation to establish proper seals without damaging raw materials. PLA demonstrates lower machine compatibility during sealing and curling operations on high-speed equipment. System setup requires increased tuning and debugging adjustments.
High-speed paper cup machines handle paperboard weights between 170 to 350 g/m² (gsm). You calculate paper thickness using a standard formula: Paper Thickness (mm) = GSM x Paper Bulkness x 0.01. Applying a paper bulkness factor of 0.14 to 0.16, 170 GSM yields 0.238 mm minimum thickness. 350 GSM yields 0.560 mm maximum thickness. Your overall compatible thickness range spans approximately 0.238 mm to 0.560 mm.
markdown
Modern paper cup machines use smart computer parts. They keep your factory running fast every day. Smart controls stop costly human mistakes. They also save your raw material from going to waste. They keep machines safe from bad mechanical damage.
Programmable Logic Controllers (PLCs) run the machine. Big brands like Siemens make these smart computers. They make all moving parts work together smoothly.
PLCs check sensor signals from every machine part.
They fix heater temperatures and drive speeds fast.
HMI touchscreens show live cup counts and speeds.
Workers save product settings on digital screens easily.
Clear color touchscreens give you complete control today. Easy HMI screens display simple visual warning alerts. Workers fix heating errors or timing problems fast. Remote experts can fix software issues online safely. This smart tech keeps your factory making cups daily.
Fast factories need smart tools to check quality. Smart cameras check every cup before final packing.
Sensor Mechanism | Primary Inspection Task | Operational Action |
|---|---|---|
High-Speed CCD Cameras | Checks inner walls for stains and bad prints | Triggers air nozzle to blow cups away |
Ultrasonic Sensor Array | Checks side seams and bottom seal tightness | Sends bad cups down the scrap chute |
Optical Rim Detectors | Checks top curl shapes and round cup sizes | Stops the machine if paper jams recur |
Air jets blow ruined cups into waste bins. These fast sensors check cups without slowing production. Throwing away bad cups stops buyer leak complaints. Automatic sorting saves labor and improves cup quality.
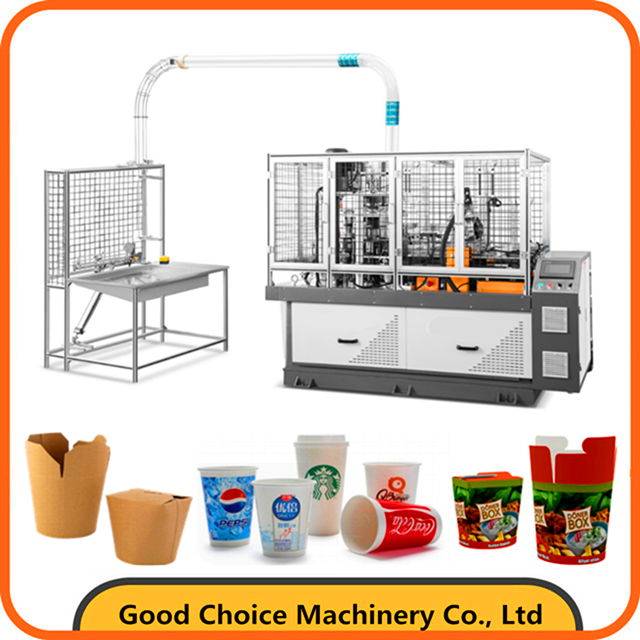
Traditional paper cup units rely on mechanical chains to transfer motion across forming stations. Heavy steel chains connect drive shafts, gears, and rotating turrets beneath the main worktable. You gain dependable power transmission at lower operational costs when you install these rugged mechanical drives. However, steel chains stretch over time through continuous mechanical friction. You must regularly adjust chain tension to prevent timing misalignment between cup-forming stations.
Chain-driven systems require frequent manual lubrication to reduce component wear. Mechanics apply grease directly to open sprockets during scheduled daily maintenance shifts. You inspect chain links routinely to prevent stretch-induced vibration during high-speed runs. Excessive chain slop leads to misaligned paper cup blanks and improper rim curling. Plant engineers select chain drives when prioritizing simple repairs over extreme high-speed tolerances.
Modern high-speed forming units utilize open-cam drive mechanics submerged in internal oil baths. Smooth cam profiles control precise mechanical arms that hold, turn, and shape paper blanks. You achieve superior precision because solid cam drives eliminate the physical backlash found in traditional chains. Lubrication pumps continuously circulate clean oil over open cams to cool heavy friction surfaces.
Automated oil systems drastically reduce manual repair hours across long production shifts. Sealed oil reservoirs catch metallic debris and filter out paper dust particles continuously. You extend the operational life of critical drive shafts by maintaining clean oil levels. Open-cam designs run quietly at elevated production speeds while maintaining exact station alignment. You protect your primary machine investment by selecting robust open-cam drive structures.
High-volume plants integrate roll-fed die-cutting machinery directly into the raw material feeding stage. Unwinding units feed giant paperboard rolls straight into automatic punching tools at continuous high speeds. Layout optimization software guides the integrated punching process to minimize paper scrap waste. Automatically driven waste stripping components clear excess paper scrap away instantly while eliminating static from raw blanks.
Conveyor tables stack and organize finished cup fans efficiently after automatic waste stripping finishes. You reduce plant floor footprints and manual labor demands by connecting die-cutters directly to forming operations. Clean paper cup blanks move smoothly toward secondary forming lines without human intervention. Integrated roll-fed die-cutting systems keep raw material supply moving without continuous operator handling.
Inline flexographic printing and die-cutting systems operate as unified automated lines, such as the RDRY-850C-4C model. The integrated system combines printing and punching operations into a single continuous process. You produce ready-to-form paper cup blanks directly from raw paper rolls within one single pass:
Raw paper rolls enter the line to initiate single-pass production.
High-definition designs are applied to single or double PE-coated paper utilizing food-grade, water-based inks.
Printed paper rolls are directly punched into cup fan shapes at high speed and stability, guided by layout optimization software to cut down paper waste.
Integrated automatic waste removal strips excess paper scraps while eliminating static from blanks.
Finished cup fans are automatically stacked and organized via conveyor tables, yielding ready-to-form blanks while minimizing floor space and manual labor.
Inline printing eliminates intermediate storage steps between printing presses and die-cutters. Water-based inks dry rapidly on single or double PE-coated surfaces before paperboard enters the punching station. You maintain strict food safety standards by utilizing non-toxic inks throughout the inline printing phase. The unified line reduces material transit risks and simplifies daily workflow management across your facility.
Automated mechanisms for counting, feeding, forming, and wrapping lower manual labor demands, directly driving down operational labor costs in manufacturing plants. Finished cups drop onto pneumatic discharge chutes immediately after top-rim curling operations finish. High-speed optical sensors count each cup accurately as air nozzles push items down transfer tubes. You eliminate manual tallying errors entirely through automated counting modules.
Full process automation operates continuously without direct manual intervention, significantly raising output volume and supporting large-scale orders. Automated processing maintains exact cup dimensions, uniform sealing quality, and standard aesthetics, effectively lowering human-induced defects. Stacking towers nest individual cups into tight, uniform sleeves before transferring them to final packing lines.
Integrated flow-wrapping units receive stacked cup sleeves directly from automatic collection conveyors. Automated pushers drive cup stacks into protective plastic films without disturbing nested cup alignments. Heat-sealing jaws trim and seal plastic wraps instantly to shield paper products from ambient moisture and dust. You maintain perfect hygiene standards by wrapping cups automatically before shipping.
Downstream packaging equipment handles high-speed cup output without creating operational bottlenecks. Flow-wrapped cup sleeves travel straight onto box-packing tables or automatic case packers. You reduce overall facility packaging costs while protecting pristine cup rims from shipping damage. Connecting forming units directly to flow-wrapping machinery optimizes your entire manufacturing equipment setup.
You must prepare your factory with strong power. High-speed cup machines need steady electrical current. You need three-phase electrical power for motors. Voltage changes damage sensitive PLC controllers fast.
Your factory layout needs dedicated power breakers. You track heating and drive power daily. Electric heaters draw constant current for heat. Good power planning stops major electrical overloads.
Pneumatic systems drive essential moving cup parts. You need air compressors for cup ejectors. Clean, dry air protects delicate air valves.
Your plant must keep constant air pressure. Pressure drops cause cup ejection failures quickly. You install air filters to remove oil. Regular system maintenance stops costly machine downtime.
Design your factory floor for easy work. High-speed cup machines need open room. Clear wide paths around each machine today.
Workers need safe zones to handle paper. Restricted work space slows down mold changes. Put control touchscreens in clear view. Good floor space keeps lines safe today.
Smooth material movement stops factory floor supply bottlenecks. Store paper blanks near the feeding stations. Forklifts need open paths to move paper.
Stage finished goods near packaging areas fast. Fast workflows stop clutter around stacking stations. Organized pathways protect raw paperboard from damage.
Traditional side-seam sealing uses electric heat. Heating jaws press paperboard edges together.
Metric / Aspect | Electric Heater Sealing | Ultrasonic Side-Sealing |
|---|---|---|
Energy Operation Mode | Continuous power draw throughout shifts to maintain set temperature. | On/off intermittent power draw (consumes electricity only during actual weld time). |
Power Consumption Example | Four 500-W cartridge heaters run continuously at 32,000 W/day. | Peak rating of 1,500 W, but draws power for only ~20 seconds per minute (weld bursts ~200 ms). |
Energy Savings | Baseline reference. | Consistently achieves at least 25% lower energy usage compared to thermal sealing. |
Sealing Speed & Rates | Slower cycles due to required cooling/set-up times; potential machine slowdowns to handle hot tack. | Rapid completion in 150 ms; capable of reaching speeds up to 110 packages/min without needing cooling periods. |
Electric heat systems need preheating time first. Continuous thermal exposure causes hot tack issues.
Ultrasonic side-sealing provides efficient bond strength fast.
Ultrasonic tools require zero warmup time.
Direct sealing finishes in 100 milliseconds.
Ultrasonic tools seal through product residue fast.
Cold tooling prevents damaging hot tack issues.
You lower power bills with ultrasonic tools. This technology handles sensitive PLA biodegradable coatings well.
Checking machine costs means looking past price tags. Smart managers calculate long-term return on investment. They study total costs over time carefully. Strong machines must offer great durability. That keeps your daily shifts making money.
Focusing on low prices causes quick line breakdowns. Tough frames and hard steel parts stop wear. Buying strong machines cuts lifetime costs fast. It also keeps your factory output very stable.
First costs are just one small step. Cheap machines have lower upfront costs. But light metal parts break down very fast. Top machines use strong iron frames. Those frames absorb hard machine shakes easily.
You lower unit costs with reliable tools. Tough machines stay straight for years. Strong structures stop constant machine failures. They protect your money during fast work shifts.
Shipping fees change your total budget quickly. Freight costs, taxes, and port fees add up. You must plan for these extra costs early. Do this during your gear buying phase.
Factory setup needs careful planning before tools arrive. Pro crews must bolt heavy frames down tight. They use strong concrete floors for stability. Proper leveling stops frame twists and saves parts.
Fast-wearing parts need fast fix schedules. This stops sudden work shutdowns on your floor. Paper grippers, heaters, and curling dies wear out. They face hard friction every single day. Track part lifespans to stop paper waste.
Keep key spare parts inside your shop. Ordering rare parts takes way too long. That can stop your work for weeks. Standard parts keep repair costs very low. They make your spending easy to predict.
Unplanned stops kill your plant profits fast. Regular care stops bad machine breakdowns. Do this before big work runs start. Workers must check oil levels every day. They must also clean out paper dust.
Tracking machine care helps spot bad trends early. Modern plants fix small problems during paper changes. Good repair habits keep your output high. They protect costly drive systems from damage.
Check seller deals and service contracts well. Good warranties cover drives and cams. They cover main frames for one year. Get fast service promises in your contract.
Good sellers give fast help online. They connect right to smart machine controls. Remote tech staff fix software issues fast. Good service protects your machine investment well. It stops costly factory delays quickly.
Seller techs must build your gear on-site. They run tests inside your factory building. Smart engineers set up proper sealing heat. They test your specific paper board stock. Good setup ensures machines run safely fast.
Full training builds team skill fast. Techs teach staff key safety steps today. Workers learn mold changes and care skills. Skilled workers run tools without making mistakes.
Buying heavy tools needs clear plans and test steps. You must guard your money before buying machines. A good plan fits your technical goals to work.
You must group your buying needs into clear categories. A full list stops costly setup mistakes. It helps you pick good sellers. You build this plan around your market and budget.
Parameter Category | Key Checklist Items | Strategic Importance |
|---|---|---|
Material & Product Specs | - Cup sizes & target markets | Sets mold needs and paper fit. |
Operational & Layout | - Expected daily/monthly output | Prepares rooms and fits machine speed. |
Financial & Testing | - Startup budget (molds, raw materials, spares) | Stops extra costs and checks cup quality. |
Your price request must list technical needs for sellers. Clear papers help you check competing deals.
Technical Specifications & Performance: The request must list speed, scrap rates, and mold change times.
Total Cost of Ownership (TCO): Check 5-year costs including price, power needs, and spare parts.
Compliance & Acceptance: Check CE or UL rules. Link payments to delivery, setup, and final tests.
You must run a strict test at the shop. Do this before final shipping. You inspect the build of your paper cup manufacturing equipment. Engineers check frame strength, safety guards, and electric wires. You check air lines for leaks and test sensors.
The test checks real machine power under real stress. You run tools fast with real paper blanks. Techs check side seals, bottom curls, and top rims. You count scrap and check heat over long runs. You approve shipping only after tools pass all tests.
You build a profitable paper cup business easily. Just balance speed, materials, and startup costs. Good sellers help protect your business. They offer strong service and technical support. Switching to modern paper cup machinery works well. It cuts total power use by 30%. This lowers operating costs by a lot.
Follow a simple buying plan today. First, ask suppliers for clear machine details. Next, test machines to check real speed. Finally, prepare your plant power, air, and room. These simple steps ensure a smooth setup. They also bring long-term success to your factory.
Standard fast units handle 170 to 350 g/m² paper. This range equals 0.238 mm to 0.560 mm thickness. Match your molds to paper thickness.
A skilled team swaps molds under 20 minutes. Modern machines use slide-out drawers to speed work up.
Ultrasonic tools need zero warmup time. They seal sides in 100 milliseconds. This tech saves 25% energy over heaters. It protects heat-sensitive PLA eco-coatings well.
Rated speed is ideal top output. For example, 80 cups every minute. Actual yield shows real daily shift work. Machines yield 65 to 70 cups. Fixes, paper flaws, and care cut output.
Fast cameras and detectors scan cups continuously. They spot bad walls and distorted rims. Air jets blow ruined cups out fast. Production keeps running without slowing down.
Modern fast units use open oil-cam drives. Sealed tanks continuously pump clean oil around. This cuts manual repair hours by 80%. Loose, stretching chains need constant grease.